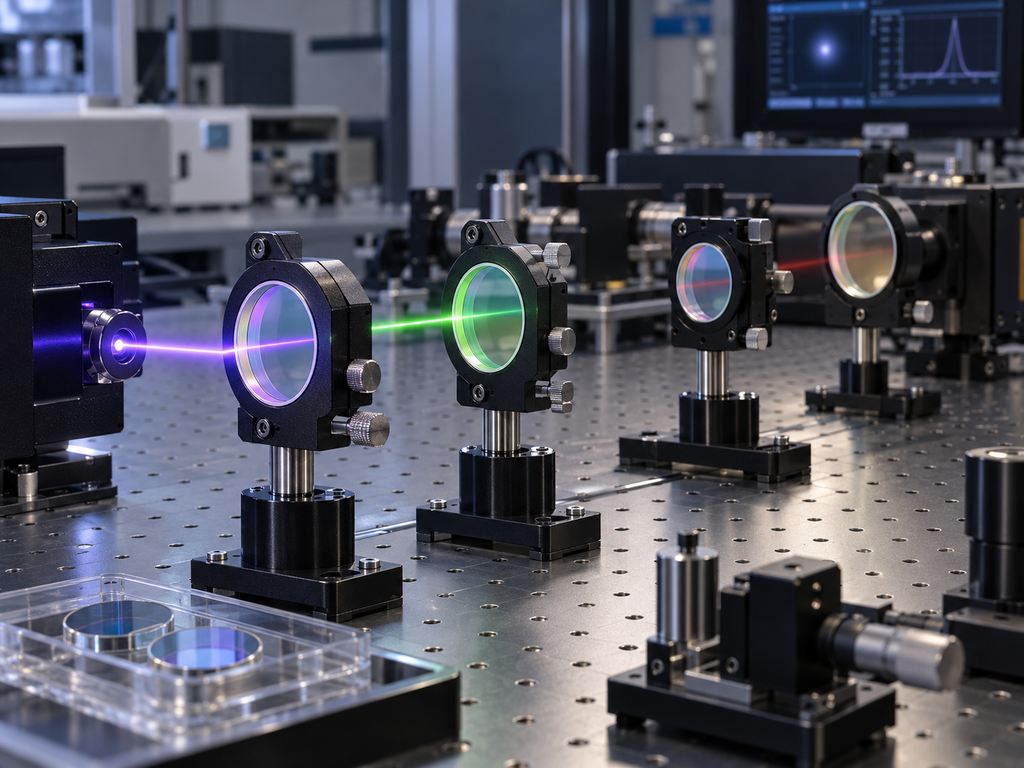
A sapphire window may have excellent mechanical strength, high hardness and good optical transmission, but in a laser system the substrate alone does not determine performance.
For many applications, the anti-reflection coating becomes one of the most critical parts of the optical design.
A coating specified incorrectly can result in:
- Excessive reflection loss
- Reduced laser transmission
- Ghost reflections
- Thermal loading
- Polarization-dependent performance
- Lower laser-induced damage threshold
- Premature coating failure
This becomes especially important at common laser wavelengths such as 355 nm, 532 nm, 1064 nm and 1550 nm.
Although all four wavelengths can use sapphire as an optical window material, the optimum coating design can be very different.
A correct coating specification therefore requires more than writing:
AR Coating @ 1064 nm
on a drawing.
The laser wavelength, angle of incidence, polarization, spectral bandwidth, pulse duration, repetition rate, beam diameter and required laser damage resistance should all be considered before the coating is designed.
Why Use AR Coatings on Sapphire Windows?
Sapphire has a relatively high refractive index compared with air.
As a result, an uncoated sapphire surface produces noticeable Fresnel reflection.
Because an optical window has two major surfaces, reflection losses from both surfaces can reduce system transmission significantly.
An anti-reflection coating is designed to reduce this surface reflection within a defined wavelength range.
For laser systems, this can provide several benefits:
- Higher transmitted laser power
- Lower back reflection
- Reduced stray light
- Improved detector signal
- Better system efficiency
- Reduced unwanted cavity effects
- Better beam stability
However, lower reflection is only one part of the design.
For high-power or pulsed lasers, coating durability and laser-induced damage threshold may be equally important.
355 nm Sapphire Window Coatings
355 nm is commonly generated as the third harmonic of a 1064 nm laser.
It is widely used in applications such as:
- UV laser micromachining
- Semiconductor processing
- PCB processing
- Glass processing
- Laser marking
- Precision ablation
- Inspection systems
UV coatings are generally more demanding than coatings for longer wavelengths.
At 355 nm, small amounts of absorption or contamination can become important because local heating and defect absorption may contribute to laser damage.
Key Coating Considerations at 355 nm
A 355 nm sapphire window may require:
- Narrowband AR coating centered near 355 nm
- Very low coating absorption
- High-purity coating materials
- Controlled coating defects
- High surface cleanliness
- Suitable laser damage resistance
Surface preparation before coating is especially important.
Residual polishing compound, organic contamination, microscopic defects or improper cleaning can reduce the power-handling capability of the finished optic.
UV Coating Durability
A coating that performs well at low optical power is not automatically suitable for high-energy UV laser operation.
UV photons place demanding requirements on coating material selection.
If the window will be exposed to:
- High pulse energy
- High repetition rate
- Short pulse duration
- Contaminated industrial environments
the coating should be designed specifically for those conditions.
For demanding 355 nm systems, LIDT testing under conditions similar to the final application may be more meaningful than relying only on a generic coating specification.
532 nm Sapphire Window Coatings
532 nm is commonly associated with frequency-doubled Nd and related solid-state laser systems.
Typical applications include:
- Green laser processing
- Laser alignment
- Biomedical equipment
- Metrology
- Imaging
- Inspection
- Research lasers
- Laser displays
- Optical sensing
Compared with 355 nm, coating material selection at 532 nm is generally less constrained by UV absorption.
However, high-energy pulsed systems still require careful attention to coating quality and defects.
Narrowband AR at 532 nm
For a single-wavelength laser, a narrowband AR coating centered at 532 nm is often the most efficient solution.
Compared with a broadband coating, a narrowband design may offer:
- Lower reflection at the target wavelength
- Simpler optimization
- Potentially better high-power performance
- Reduced unnecessary coating complexity
If the laser operates only around 532 nm, there is usually little reason to specify a very broad spectral range unless another optical function requires it.
1064 nm Sapphire Window Coatings
1064 nm is one of the most important industrial laser wavelengths.
It is widely used in:
- Nd lasers
- Fiber lasers
- Laser cutting
- Laser welding
- Laser cleaning
- Laser marking
- Semiconductor processing
- Scientific laser systems
- Rangefinding
- Industrial sensing
For high-power laser systems, 1064 nm sapphire windows can require especially careful coating selection.
The sapphire substrate may tolerate harsh mechanical environments extremely well, while the AR coating becomes the limiting factor in power handling.
High-Power 1064 nm Applications
For high-power CW lasers, engineers should consider:
- Average laser power
- Beam diameter
- Power density
- Coating absorption
- Thermal lensing
- Window cooling
- Contamination
For pulsed lasers, additional parameters become important:
- Pulse energy
- Pulse duration
- Repetition rate
- Peak fluence
- Beam profile
A coating suitable for a moderate-power CW laser should not automatically be assumed suitable for a nanosecond or picosecond system.
1550 nm Sapphire Window Coatings
1550 nm is widely used in:
- LiDAR
- Laser rangefinding
- Optical communication
- Fiber-optic systems
- Industrial sensing
- Remote sensing
- Imaging systems
- Laser measurement equipment
Sapphire can be useful where the optical window also requires high mechanical strength, scratch resistance or environmental durability.
For a 1550 nm laser window, a narrowband AR coating can be optimized specifically around the operating wavelength.
Broadband coatings may also be appropriate if the same window is used for both laser transmission and imaging.
355 nm vs 532 nm vs 1064 nm vs 1550 nm
A simplified selection comparison is shown below.
| Laser Wavelength | Typical Applications | Main Coating Concern |
|---|---|---|
| 355 nm | UV micromachining, semiconductor processing, ablation | UV absorption, contamination, coating defects, LIDT |
| 532 nm | Green lasers, inspection, metrology | Low reflection, pulsed-laser durability |
| 1064 nm | Cutting, welding, marking, fiber/Nd systems | High-power handling, LIDT, thermal stability |
| 1550 nm | LiDAR, sensing, rangefinding, communications | Low reflection, AOI, environmental durability |
This table is only a starting point.
The actual coating design must still consider laser operating conditions.
Narrowband vs Broadband AR Coatings
One of the first decisions when specifying a sapphire laser window is whether the coating should be narrowband or broadband.
Narrowband AR Coating
A narrowband coating is optimized around one laser wavelength.
Examples include:
- AR @ 355 nm
- AR @ 532 nm
- AR @ 1064 nm
- AR @ 1550 nm
This approach is usually appropriate when the system operates at a single defined laser wavelength.
Advantages may include:
- Very low reflectance at the target wavelength
- Efficient coating optimization
- Potentially fewer coating layers
- Better suitability for high-power applications
The exact performance depends on the coating design.
Broadband AR Coating
A broadband coating is designed to reduce reflection over a wider spectral range.
Examples might include:
- 400–700 nm
- 650–1050 nm
- 900–1700 nm
Broadband coatings are useful when the sapphire window must transmit:
- Multiple wavelengths
- Imaging light
- Broadband illumination
- A laser plus observation wavelength
- Multiple laser sources
However, increasing coating bandwidth usually makes the optical design more complex.
For high-energy laser systems, unnecessarily broad bandwidth should therefore be avoided unless the application truly requires it.
Dual-Wavelength Coatings
Some systems require two discrete laser wavelengths rather than one continuous broadband range.
Typical combinations can include:
- 532 nm + 1064 nm
- 355 nm + 532 nm
- 1064 nm + another monitoring wavelength
In these cases, a dual-band AR design may be more appropriate than a broadband coating.
When requesting such a coating, specify both wavelengths and their relative importance.
Angle of Incidence: Why AOI Must Be Specified
Many AR coating specifications assume near-normal incidence.
But not every sapphire window is installed perpendicular to the laser beam.
If the window operates at an angle, coating performance changes.
This is why AOI — Angle of Incidence — should be included in the RFQ.
Typical specifications might be:
AOI: 0°
or
AOI: 45°
or
AOI: 0–10°
At oblique incidence, the spectral response of a multilayer coating shifts, and the behavior of S and P polarization can become different.
A coating optimized for 1064 nm at normal incidence may therefore not provide the same performance at 45° incidence.
AOI and Spectral Shift
As the angle of incidence increases, the effective optical thickness of coating layers changes.
As a result, the AR performance generally shifts toward shorter wavelengths.
For systems with a significant AOI, the coating should therefore be designed for the actual operating angle rather than simply using a standard normal-incidence coating.
AOI and Polarization
At normal incidence, polarization effects are relatively small.
At larger angles, S-polarized and P-polarized light behave differently.
This means a coating specification may need to define:
- S polarization
- P polarization
- Unpolarized light
- Mixed polarization
This is particularly relevant for precision laser systems and 45-degree optical windows.
Why LIDT Cannot Be Specified by Wavelength Alone
Laser-Induced Damage Threshold, or LIDT, is one of the most important specifications for high-power laser optics.
However, an LIDT value without test conditions is incomplete.
For example:
LIDT > 10 J/cm²
is not sufficient information by itself.
The damage behavior of an optic can depend on:
- Wavelength
- Pulse duration
- Pulse repetition rate
- Beam diameter
- Beam profile
- Number of pulses
- Polarization
- AOI
- Surface quality
- Coating design
- Surface cleanliness
Therefore, two LIDT values measured under different test conditions cannot necessarily be compared directly.
Pulsed Laser LIDT
For pulsed lasers, LIDT is often expressed in:
J/cm²
But the pulse duration matters greatly.
A nanosecond laser and a femtosecond laser can have completely different damage mechanisms.
The RFQ should therefore include, where relevant:
- Wavelength
- Pulse energy
- Pulse width
- Repetition rate
- Beam diameter
CW Laser Damage
For continuous-wave lasers, average power and thermal behavior become more important.
Relevant information can include:
- Laser power in watts
- Beam diameter
- Power density
- Exposure duration
- Cooling conditions
- Window mounting
Absorption in the coating or substrate can cause localized temperature increase.
Even very small absorption levels can become significant in high-power laser systems.
ISO 21254 and LIDT Testing
For applications requiring formal laser damage qualification, ISO 21254 provides an important framework for testing laser-induced damage of optical components.
When comparing LIDT data from different suppliers, ask:
- Which test method was used?
- At what wavelength?
- What was the pulse duration?
- What beam size was used?
- Was the test 1-on-1 or S-on-1?
- Which surface was tested?
- Was the optic coated?
- What damage criterion was used?
Without this information, a large LIDT number can be misleading.
The Coating Can Fail Before the Sapphire
Sapphire itself is mechanically robust and can provide excellent environmental durability.
In many laser applications, however, the thin-film coating is more sensitive than the substrate.
Potential coating failure mechanisms include:
- Local thermal damage
- Pinpoint laser damage
- Delamination
- Microcracking
- Surface contamination
- Humidity-related degradation
- Abrasion
- Cleaning damage
Therefore, a sapphire window described simply as “high-power laser grade” still requires a clear coating specification.
Surface Quality and LIDT
Coating performance begins with the substrate surface.
Potential damage initiation sites include:
- Polishing defects
- Scratches
- Dig defects
- Subsurface damage
- Particles
- Organic contamination
- Coating nodules
- Local absorption sites
For demanding laser applications, surface preparation and cleanliness can influence LIDT as much as the theoretical coating design.
A tighter scratch-dig specification may be appropriate for high-power laser optics, but scratch-dig alone does not fully describe laser damage performance.
Surface roughness, subsurface condition and cleanliness should also be considered.
Cleaning Sapphire Laser Windows
Sapphire is highly scratch resistant, but the coating may not have the same mechanical durability.
This distinction is important during maintenance.
An uncoated sapphire surface can tolerate handling conditions that could damage a thin-film AR coating.
Cleaning procedures should therefore consider:
- Coating material
- Approved solvents
- Wipe material
- Particle removal method
- Mechanical pressure
- Cleaning frequency
Avoid assuming that sapphire’s Mohs 9 hardness applies to the coating.
It does not.
Environmental Durability
Some sapphire laser windows are installed in controlled laboratory environments.
Others operate in:
- Industrial laser cutting systems
- Laser welding heads
- Outdoor LiDAR
- Aerospace sensors
- Vacuum systems
- High-temperature equipment
- Dusty manufacturing environments
The coating design should consider the actual environment.
Potential durability requirements include resistance to:
- Humidity
- Temperature cycling
- Abrasion
- Salt atmosphere
- Dust
- Cleaning chemicals
- Vacuum exposure
A coating optimized only for minimum reflectance may not be the best choice for an industrial protective window.
Single-Side vs Double-Side AR Coating
Sapphire windows can be coated on one or both major surfaces.
Double-Side AR
Double-sided AR coating is often selected when maximizing transmission and minimizing reflection are the primary goals.
It can reduce reflection at both sapphire-air interfaces.
Single-Side AR
Single-sided coating may be useful when one surface faces a harsh environment.
For example, in an industrial laser system the external surface may be exposed to:
- Metal spatter
- Dust
- Cleaning
- Chemical contamination
Depending on the optical requirements, keeping the exposed surface uncoated may improve practical durability.
The protected surface can then carry the AR coating.
This is a system-level decision rather than a universal rule.
Protective Sapphire Windows in Laser Processing
In laser welding, cutting and cleaning systems, the sapphire window may function primarily as a protective optic.
Its purpose is to protect more expensive internal components from:
- Spatter
- Smoke
- Dust
- Debris
- Process contamination
In these applications, coating selection must balance:
Optical efficiency vs service-life cost.
A coating with extremely low reflection but poor resistance to repeated cleaning may not be the most economical solution.
Crystal Orientation Can Also Matter
Sapphire is an anisotropic single crystal rather than an isotropic glass.
For many standard protective windows, crystal orientation may not significantly affect the practical system.
However, polarization-sensitive or precision optical applications may need to consider birefringence and crystal orientation.
C-plane sapphire is commonly used for optical windows, but the final orientation should be selected based on:
- Optical geometry
- Polarization
- Mechanical design
- Thermal requirements
If polarization behavior is critical, this should be stated in the RFQ.
How to Specify a 355 nm Sapphire Window
A useful RFQ might include:
Material: Optical-grade single-crystal sapphire
Wavelength: 355 nm
AOI: 0°
Coating: AR @ 355 nm, both surfaces
Laser type: Pulsed UV laser
Pulse duration: Specify value
Repetition rate: Specify value
Pulse energy: Specify value
Beam diameter: Specify value
Surface quality: As drawing
Clear aperture: As drawing
LIDT: Required/tested under specified conditions
This provides much more useful information than simply requesting:
355 nm AR sapphire window.
How to Specify a 532 nm Sapphire Window
Example:
Material: Sapphire
Operating wavelength: 532 nm
AOI: 0–5°
Polarization: Specify if applicable
AR coating: Low reflectance at 532 nm
Laser mode: CW or pulsed
Laser power/energy: Specify
Clear aperture: Specify
Environmental requirement: Indoor industrial equipment
How to Specify a 1064 nm High-Power Sapphire Window
For high-power applications, include more laser data.
Example:
Material: Optical sapphire
Wavelength: 1064 nm
Laser type: Fiber laser / Nd
Operation: CW or pulsed
Maximum power: Specify
Pulse width: If pulsed
Repetition rate: If pulsed
Beam diameter: Specify
AOI: Specify
Coating: High-LIDT AR @ 1064 nm
Cooling: Describe if relevant
Clear aperture: Specify
The optical manufacturer can then evaluate whether a standard laser coating is adequate or a custom high-LIDT coating is required.
How to Specify a 1550 nm Sapphire Window
Example:
Application: LiDAR / rangefinder
Material: Optical-grade sapphire
Wavelength: 1550 nm
AOI: 0–20° or specified working angle
Polarization: Unpolarized or specified
AR coating: Optimized around 1550 nm
Environmental condition: Outdoor / industrial
Surface durability: Specify
Clear aperture: Specify
For LiDAR systems with a wide field of view, AOI range may be particularly important.
Common Coating Specification Mistakes
Mistake 1: Only Specifying the Wavelength
“AR@1064 nm” does not define AOI, bandwidth, reflectance or power-handling requirements.
Mistake 2: Ignoring AOI
A coating designed at 0° may perform differently at 30° or 45°.
Mistake 3: Asking for Maximum Bandwidth Without Need
Broader is not automatically better.
For a single laser wavelength, narrowband AR may be the more practical choice.
Mistake 4: Using an LIDT Number Without Test Conditions
LIDT values are meaningful only when the relevant laser and test parameters are known.
Mistake 5: Assuming the Coating Is as Hard as Sapphire
Sapphire is extremely hard.
Thin-film coatings can still be scratched or damaged during cleaning.
Mistake 6: Ignoring the Second Surface
A two-surface window can produce multiple reflections and ghost beams.
Both surfaces should be considered in the optical design.
Recommended RFQ Information
When requesting a coated sapphire laser window, provide as many of the following parameters as possible:
| Parameter | Information to Provide |
|---|---|
| Sapphire dimensions | Diameter, length, width and thickness |
| Crystal orientation | If required |
| Operating wavelength | 355, 532, 1064, 1550 nm or custom |
| Spectral range | Narrowband, dual-band or broadband |
| AOI | Nominal angle and tolerance/range |
| Polarization | S, P, unpolarized or variable |
| Reflectance requirement | Per surface or total |
| Laser type | CW or pulsed |
| Average power | For CW/high-duty systems |
| Pulse energy | For pulsed systems |
| Pulse duration | ns, ps, fs, etc. |
| Repetition rate | Hz, kHz, MHz, etc. |
| Beam diameter | At the sapphire window |
| LIDT requirement | Including test conditions |
| Surface quality | Scratch-dig requirement |
| Flatness | If required |
| Clear aperture | Optical usable area |
| Coating sides | One side or both sides |
| Environment | Indoor, outdoor, vacuum, high temperature, etc. |
| Quantity | Prototype and production quantity |
Frequently Asked Questions
Does sapphire need an AR coating for laser applications?
Not always, but an AR coating can significantly reduce surface reflection and improve transmission. Whether it is necessary depends on acceptable system loss and back-reflection requirements.
Which coating is best for a 1064 nm sapphire window?
For a laser operating only around 1064 nm, a narrowband AR coating optimized for the actual AOI is often a practical choice. For high-power systems, LIDT and absorption should also be considered.
Can one sapphire window work at both 532 nm and 1064 nm?
Yes. A dual-band coating can be designed for both wavelengths if required. This should be specified when requesting the coating.
Can broadband AR coating be used for high-power lasers?
It can, but broadband performance and high LIDT are separate requirements. If only one wavelength is used, an unnecessarily broad coating may add complexity without providing practical benefit.
Does AOI affect AR coating performance?
Yes. Increasing AOI changes the coating’s spectral response and increases the difference between S- and P-polarized light. Coatings should therefore be designed for the actual working angle.
What does LIDT mean?
LIDT means Laser-Induced Damage Threshold. It describes the laser irradiation level associated with damage onset under defined test conditions. It should always be interpreted together with wavelength, pulse duration, repetition rate, beam size and test method.
Is sapphire itself more durable than the AR coating?
Mechanically, this is often the case. Sapphire is extremely hard and wear resistant, but the thin-film coating may be more sensitive to scratching, contamination, thermal stress and laser damage.
Should both sides of a sapphire window be AR coated?
For maximum optical transmission, both surfaces are commonly coated. However, if one surface is exposed to severe contamination or repeated mechanical cleaning, a single-side coating strategy may sometimes be considered.
Can a sapphire window be coated for 355 nm, 532 nm, 1064 nm and 1550 nm simultaneously?
A very broad or multi-band coating may be technically possible depending on the required performance, but it is usually better to specify the actual wavelengths and acceptable reflectance rather than requesting the broadest possible range.
Conclusion
Selecting an AR coating for a sapphire laser window requires much more than matching a coating to a wavelength.
A successful coating design must consider:
- 355 nm, 532 nm, 1064 nm or 1550 nm operating wavelength
- Narrowband, dual-band or broadband requirements
- Angle of incidence
- Polarization
- Laser power or pulse energy
- Pulse duration
- Repetition rate
- Beam diameter
- LIDT
- Surface preparation
- Environmental durability
- Cleaning requirements
For low-power applications, optical transmission may be the primary consideration.
For high-power laser systems, the limiting factor may instead be coating absorption, contamination, defects or laser-induced damage.
The most reliable approach is therefore to provide the sapphire window manufacturer with both the mechanical drawing and the actual laser operating parameters.
When requesting a custom coated sapphire window, include the wavelength, AOI, polarization, laser power or pulse conditions, clear aperture, surface specifications and environmental requirements.
This allows the coating to be designed for the real optical system rather than simply applying a generic AR coating to a sapphire substrate.