Large-aperture sapphire windows are increasingly used in electro-optical and infrared systems where a sensor requires both high optical transmission and strong environmental protection.
Typical non-military applications include:
- industrial thermal imaging;
- high-temperature process monitoring;
- semiconductor equipment;
- gas detection;
- scientific instruments;
- environmental monitoring;
- machine vision;
- infrared spectroscopy;
- high-power optical systems;
- harsh-environment cameras.
For small optical windows, engineers may focus mainly on wavelength, diameter and coating.
As aperture increases, however, the window becomes an important structural element.
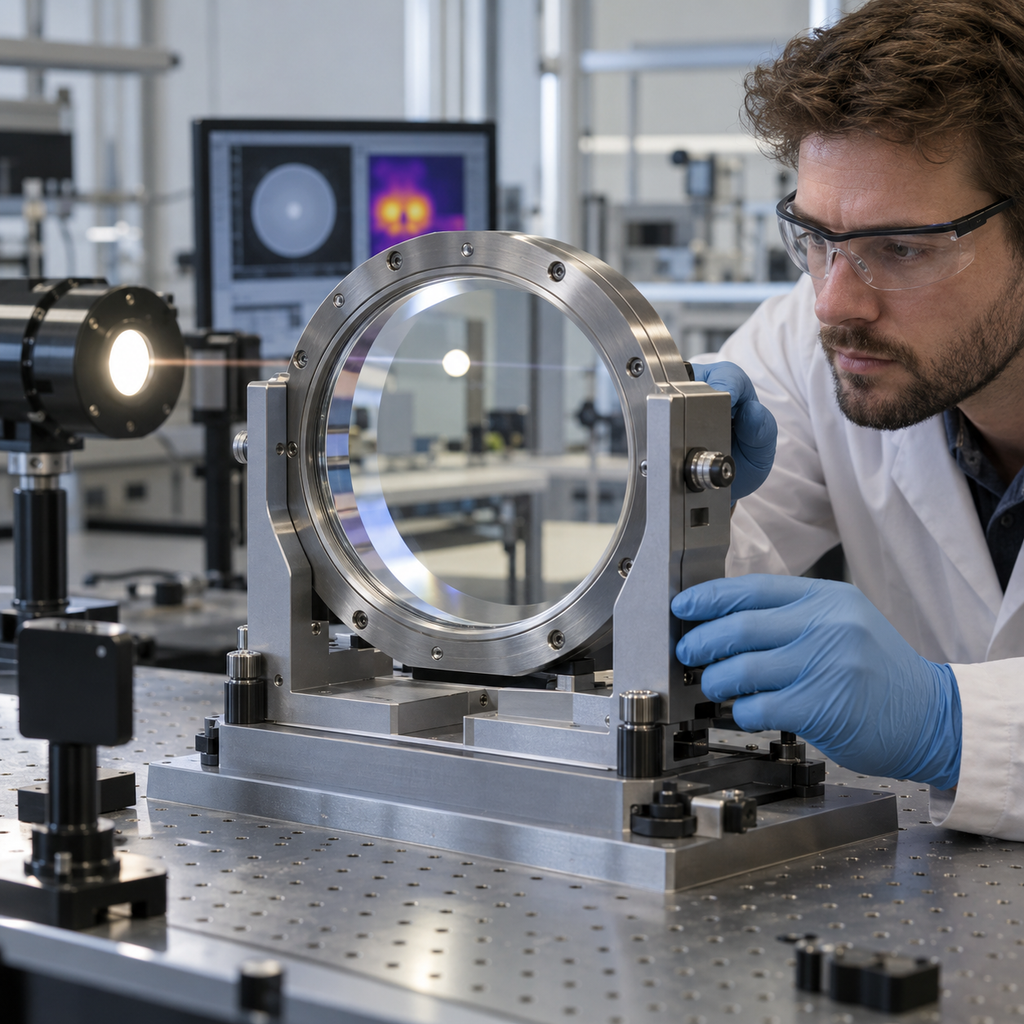
A large sapphire window must simultaneously control:
optical transmission
→ thickness
→ flatness
→ transmitted wavefront
→ gravity sag
→ mounting stress
→ edge strength
→ thermal expansion
→ coating stress
→ inspection accuracy
This is why a large-aperture sapphire window should not simply be designed as an enlarged version of a smaller optical disc.
1. What Is a Large-Aperture Sapphire Window?
There is no single industry diameter that defines a “large-aperture” sapphire window.
From a practical optical-fabrication perspective, the term generally becomes relevant when increasing size begins to affect:
- polishing difficulty;
- material cost;
- surface figure;
- thickness;
- mechanical deformation;
- mounting;
- inspection.
Commercial sapphire windows are available in diameters reaching approximately 150 mm, with current catalog examples providing around 135 mm clear aperture.
Custom windows can also use:
- circular shapes;
- rectangular shapes;
- square windows;
- elongated apertures;
- stepped profiles;
- custom edge geometries.
For industrial EO/IR sensor systems, the important dimension is not necessarily overall diameter.
The more useful dimension is often:
Clear Aperture
because this defines the optical region through which the sensor collects radiation.
2. Why Sapphire Is Used for EO/IR Sensor Windows
Sapphire is single-crystal aluminum oxide:
Al₂O₃
Its combination of mechanical and optical properties makes it useful where ordinary optical glass is too fragile.
Key advantages include:
- extreme hardness;
- high stiffness;
- good mechanical strength;
- good thermal conductivity;
- resistance to abrasion;
- chemical resistance;
- broad optical transmission.
Commercial sapphire windows can transmit from approximately the near-UV through visible and well into the infrared, with standard optical products commonly specified across approximately 330–5500 nm.
That makes sapphire useful for systems combining:
- visible imaging;
- near-IR sensing;
- SWIR;
- portions of MWIR.
For a sensor located in a harsh industrial environment, the outer sapphire window can protect much more sensitive optics behind it.
3. Large Aperture Changes the Mechanical Problem
Consider two sapphire windows:
Window A
Diameter: 25 mm
Window B
Diameter: 150 mm
The second window has six times the diameter.
But its area is approximately:
6² = 36 times greater.
Therefore a uniform pressure load or environmental force acts over a much larger area.
At the same time, a larger plate is much more sensitive to bending.
This is why large-window thickness cannot be scaled linearly with diameter.
Important variables include:
- unsupported diameter;
- thickness;
- support geometry;
- pressure differential;
- gravity direction;
- temperature gradient;
- edge condition.
A large window may be optically excellent while resting freely on an interferometer but deform significantly after installation into a rigid housing.
4. Outside Diameter Is Not the Same as Clear Aperture
A typical drawing may contain three different diameters:
Outside Diameter
The physical size of the sapphire component.
Support Diameter
The region contacted by the mounting structure.
Clear Aperture
The usable optical region.
For example:
Outside Diameter: 150 mm
Support Diameter: 142 mm
Clear Aperture: 130 mm
These values should not be confused.
Mechanical bending is strongly influenced by the unsupported diameter, while optical system performance depends on the clear aperture.
Therefore an RFQ saying:
Need Ø150 mm sapphire window
is incomplete.
A supplier also needs to know:
What is the clear aperture?
5. Thickness Design
Window thickness influences both mechanical and optical performance.
Increasing thickness generally improves:
- stiffness;
- pressure resistance;
- resistance to deflection;
- handling strength.
But thicker sapphire also increases:
- material cost;
- weight;
- optical path length;
- manufacturing time;
- potential absorption at longer IR wavelengths.
The optimal thickness is therefore a compromise.
Commercial sapphire components illustrate that thickness can vary greatly depending on application. For example, 25 mm sapphire windows are available at only 0.5 mm thickness, while larger 150 mm windows may use several-millimeter thicknesses.
These catalog examples should not be interpreted as universal structural design rules.
The required thickness depends on the real mounting condition.
6. Thickness-to-Diameter Ratio
The ratio:
t / D
where:
- t = thickness;
- D = unsupported diameter
is a useful conceptual indicator of window stiffness.
As D increases without a corresponding thickness increase, bending sensitivity increases rapidly.
However, there is no universal t/D value for sapphire windows because the correct design depends on:
- pressure;
- optical wavefront requirement;
- material orientation;
- support condition;
- safety factor;
- environmental temperature.
For a protective sensor window exposed only to atmospheric conditions, one thickness may be sufficient.
For a vacuum or pressurized system using the same diameter, a much larger thickness may be required.
7. Flatness Becomes Harder as Aperture Increases
Surface flatness describes deviation from an ideal plane.
Typical specifications include:
- 1λ;
- λ/2;
- λ/4;
- λ/10.
The test wavelength should always be specified.
Commonly:
632.8 nm
is used for visible interferometric testing.
For larger sapphire windows, achieving tight flatness becomes progressively harder because:
- more material must be polished uniformly;
- polishing pressure varies across the aperture;
- residual stress becomes more important;
- gravity can deform thin parts during measurement;
- coating can change the final surface figure.
Large or thin sapphire windows are particularly sensitive to support conditions during interferometric inspection. Your inspection method should therefore control fixture pressure and gravity orientation.
8. Flatness Is Not the Same as Transmitted Wavefront
This distinction is particularly important for EO/IR imaging.
Surface flatness measures:
the shape of one optical surface.
Transmitted wavefront error measures:
the optical distortion created after light passes through the entire window.
A window can have two individually good surfaces but still produce optical distortion because of:
- wedge;
- thickness variation;
- internal refractive-index variation;
- mounting stress;
- coating stress.
Transmitted wavefront testing evaluates the complete component and is particularly useful for:
- high-resolution imaging;
- optical metrology;
- precision sensors;
- laser systems.
For demanding EO/IR systems, it can therefore be more meaningful to specify:
Transmitted Wavefront ≤ λ/4
instead of only:
Surface Flatness ≤ λ/4
9. Why Imaging Systems Care About Wavefront Error
An imaging sensor depends on the entire optical system maintaining image quality.
If a protective window introduces wavefront distortion, it can reduce:
- image sharpness;
- contrast;
- MTF;
- focus consistency;
- detector calibration accuracy.
This becomes especially important for a large window positioned in front of a high-resolution camera.
For simple industrial observation, λ/2 flatness may be sufficient.
For high-precision imaging, customers may request:
- λ/4;
- λ/10;
- transmitted wavefront control.
The requirement should be determined from the optical error budget.
Over-specifying every industrial window at λ/10 can dramatically increase manufacturing cost.
10. Surface Roughness
Flatness describes large-scale surface shape.
Surface roughness describes microscopic surface variation.
Typical polished sapphire windows may require:
Ra < 1 nm
for precision optical systems.
Low roughness helps reduce:
- optical scattering;
- haze;
- coating defects;
- stray light.
This can be especially important in:
- infrared detection;
- low-light imaging;
- spectroscopy;
- laser systems.
However, roughness and surface quality are different specifications.
A surface can have excellent nanometer-scale roughness while still containing a visible scratch.
11. Surface Quality
Optical surface cosmetic quality is commonly specified using scratch-dig values.
Examples include:
60/40
40/20
20/10
The application should determine the requirement.
Industrial Protective Sensor Window
60/40 or 40/20 may be sufficient.
Precision EO/IR Imaging
40/20 or 20/10 may be more appropriate.
Laser / High-Sensitivity Optical System
20/10 or tighter may be required.
Specifying 10/5 for every large sapphire window can significantly increase production difficulty.
Because the surface area increases with aperture, maintaining extremely tight cosmetic requirements becomes more difficult on large parts.
12. Parallelism and Wedge
A parallel window ideally has two optical surfaces that remain parallel.
If the surfaces form an angle, the window has:
wedge
Wedge can produce:
- beam deviation;
- image shift;
- focus error;
- boresight change.
Commercial sapphire windows often specify parallelism in arcminutes for general applications. For example, common precision catalog windows can use parallelism around ≤3.5 arcmin.
More demanding EO/IR systems may require substantially tighter tolerances.
But in some laser systems, a small intentional wedge may actually be beneficial because it reduces:
- ghost reflections;
- etalon effects.
Therefore, “perfect parallelism” is not always the correct requirement.
13. Why Mounting Stress Is Critical
A sapphire window may be manufactured perfectly and then distorted during assembly.
This is one of the most important causes of unexpected optical problems.
Mounting stress can come from:
- over-tightened retaining rings;
- uneven screw torque;
- adhesive shrinkage;
- O-ring compression;
- metal housing expansion;
- misaligned support surfaces;
- particles trapped under the edge.
For a small thick window, these forces may create little measurable distortion.
For a large, thin sapphire window, the same mounting force can produce significant bending.
14. Never Treat Sapphire Like a Metal Cover Plate
Sapphire has very high stiffness, but it is brittle.
It does not yield plastically like aluminum or steel.
If the edge is locally overloaded, the part may:
- chip;
- crack;
- fracture suddenly.
Therefore, mounting design should distribute force as uniformly as possible.
Avoid:
- point loading;
- sharp metal contact;
- uneven screw pressure;
- hard clamping directly against optical edges.
A compliant layer or carefully designed support structure can reduce local stress.
Historical large-aperture sapphire-window development has shown that both high-quality polishing and mounting arrangement can materially affect effective window strength.
15. O-Ring Mounting
O-rings are frequently used where sealing and mechanical compliance are both required.
Advantages include:
- distributed support;
- reduced hard contact;
- sealing capability;
- accommodation of dimensional variation.
However, excessive O-ring compression can still deform a large sapphire window.
Important variables include:
- O-ring material;
- hardness;
- cross-section;
- squeeze percentage;
- groove geometry;
- temperature.
The mounting design should ensure the O-ring supports and seals the window without generating unnecessary bending force.
16. Retaining Ring Mounting
A retaining ring is another common structure.
Typical arrangement:
housing shoulder
→ compliant gasket
→ sapphire window
→ compliant gasket
→ retaining ring
This design can prevent direct sapphire-to-metal contact.
The retaining ring should not be tightened until the sapphire becomes mechanically clamped like a structural bolt joint.
Its purpose is normally to retain the window while allowing controlled thermal movement.
Torque control can be important for larger apertures.
17. Adhesive Mounting
Adhesive bonding can simplify installation.
But adhesive introduces its own risks:
- curing shrinkage;
- CTE mismatch;
- outgassing;
- aging;
- chemical compatibility.
A rigid adhesive ring around the entire circumference can transfer housing stress directly to the sapphire.
For large apertures, engineers should consider whether the adhesive requires:
- controlled bond-line thickness;
- flexible modulus;
- segmented application;
- environmental qualification.
Optical performance should ideally be inspected after final assembly.
18. Thermal Expansion Mismatch
A large sapphire window may be installed in:
- aluminum;
- stainless steel;
- titanium;
- ceramic housings.
Each material expands differently with temperature.
If a metal housing expands more than the sapphire and the window is rigidly constrained, thermal stress develops.
The larger the window diameter, the greater the absolute dimensional difference can become.
For example, the basic thermal expansion relationship is:
ΔL = α × L × ΔT
Therefore increasing:
- diameter;
- temperature excursion;
- CTE difference
increases relative displacement between window and housing.
A large-aperture mounting system should therefore normally allow some controlled radial movement.
19. Edge Strength Is Often More Important Than Bulk Strength
Sapphire has high theoretical and measured strength.
But real components usually fail from:
- edge chips;
- scratches;
- subsurface cracks;
- grinding damage.
The edge therefore deserves special attention.
A microscopic crack can create a stress concentration.
Under:
- pressure;
- mounting force;
- vibration;
- thermal cycling,
that crack may propagate.
This is why mechanical design should not rely solely on a published sapphire flexural-strength number.
Finished-part edge quality matters.
20. Edge Grinding
After sapphire is cut from a boule or blank, the edge is typically ground to final dimension.
Poor edge grinding can leave:
- large grinding marks;
- microcracks;
- chips;
- localized stress risers.
For large sensor windows, finer edge finishing may improve reliability.
RFQ terminology may include:
Fine ground edge
or:
Polished edge
depending on requirement.
Commercial optical sapphire windows often use fine-ground edges with protective bevels.
21. Edge Bevel and Chamfer
Sharp sapphire edges are vulnerable to damage.
A controlled bevel or chamfer helps protect the edge.
Examples:
0.2 × 45°
0.5 × 45°
or:
protective bevel as needed
The appropriate size depends on:
- thickness;
- diameter;
- mounting area;
- clear aperture.
The bevel should not intrude into the required optical aperture.
For rectangular sapphire windows, corner radii can serve a similar mechanical function by reducing stress concentration.
22. Maximum Edge Chip Requirement
Instead of stating:
No chips.
A better drawing requirement is measurable.
For example:
Maximum edge chip: ≤0.1 mm
or define separate:
- length;
- depth;
- position.
The drawing can also identify a critical zone around the clear aperture or sealing surface.
For large sapphire components, completely eliminating microscopic edge defects may be unrealistic and unnecessarily expensive.
A measurable acceptance criterion is better.
23. Rectangular Large-Aperture Sapphire Windows
Not every EO/IR sensor uses a circular window.
Rectangular designs are common in:
- industrial thermal cameras;
- line-scan systems;
- scientific instrumentation.
Rectangular windows create additional structural issues.
The corners can concentrate stress.
Therefore designers often use:
corner radii
instead of perfectly sharp 90° internal geometries.
Important RFQ parameters include:
- length;
- width;
- thickness;
- corner radius;
- clear aperture;
- support area.
For unusually large rectangular windows, FEA can be useful before finalizing thickness.
24. Gravity Sag
Large optical windows can deform under their own weight.
This may seem surprising because sapphire is very stiff.
But precision optical measurements can detect extremely small deformation.
Gravity sag depends on:
- diameter;
- thickness;
- mounting orientation;
- support position.
This has two important consequences.
First:
inspection fixture orientation matters.
Second:
A window used vertically in a sensor may have different deformation behavior than when measured horizontally on an interferometer.
For demanding systems, measurement orientation should resemble the final use condition as closely as practical.
25. Coating Stress
AR coatings introduce additional mechanical stress.
Multilayer coatings may contain materials with different:
- CTE;
- intrinsic stress;
- elastic properties.
For a small thick window, coating stress may be negligible.
For a large, thin window, it can change:
- flatness;
- bow;
- transmitted wavefront.
Therefore a part should ideally be inspected:
after final coating
when flatness or transmitted wavefront is critical.
Do not assume the polished pre-coating flatness will remain unchanged.
26. AR Coatings for EO/IR Systems
Bare sapphire has meaningful surface reflection because of its relatively high refractive index.
AR coatings can therefore increase transmission significantly.
Typical coating bands may include:
- visible;
- 850 nm;
- 1064 nm;
- 1550 nm;
- 1.65–3 µm;
- 2–5 µm.
Commercial sapphire data show broadband AR options extending into the 2–5 µm infrared region, with coated transmission much higher than the corresponding uncoated surface system.
For EO/IR systems, the coating specification should include:
wavelength band + AOI + average reflection/transmission
rather than simply:
AR coated.
27. Angle of Incidence Matters
Large sensor windows are not always installed normal to the optical axis.
The window may be tilted to:
- reduce reflections;
- fit mechanical geometry;
- redirect ghost images.
AR coating behavior changes with angle of incidence.
Therefore the RFQ should state:
AOI = ___°
and, where relevant:
- polarization;
- cone angle;
- spectral band.
A coating designed at 0° may behave differently at 30° or 45°.
28. Clear Aperture and Coating Zone
The drawing should define exactly where the optical specification applies.
For example:
Window OD: Ø150 mm
Clear Aperture: Ø135 mm
AR coating: Ø138 mm minimum
The outer edge may remain:
- uncoated;
- ground;
- masked.
This can reduce coating difficulty and allow mounting contact without damaging the optical coating.
Commercial 150 mm sapphire windows commonly illustrate the use of a clear aperture around 90% of overall diameter.
29. Thickness Uniformity
Even if both surfaces are nominally flat, thickness can vary.
This may be specified as:
TTV — Total Thickness Variation
or through:
parallelism / wedge
depending on the component geometry.
Thickness variation matters because it can change:
- optical path length;
- focus;
- mechanical balance;
- assembly fit.
For precision sensor windows, thickness should therefore be inspected at multiple positions rather than at one center point.
30. Crystal Orientation
Sapphire is anisotropic.
Possible orientations include:
- C-plane;
- A-plane;
- R-plane;
- M-plane.
For many optical windows, C-plane is a common choice.
Orientation can affect:
- birefringence;
- thermal expansion;
- optical properties;
- machining behavior.
For ordinary protective imaging windows, orientation may be less critical.
For polarization-sensitive EO/IR systems, it should be specified.
31. Birefringence
Unlike fused silica, sapphire is birefringent.
That means refractive index depends on polarization and crystal direction.
In normal industrial thermal imaging, this may be acceptable.
But it can matter in:
- polarization imaging;
- interferometry;
- spectroscopy;
- laser systems.
When polarization performance matters, the RFQ should state:
- crystal orientation;
- optical axis orientation;
- polarization requirements.
Do not assume that all sapphire windows are optically equivalent simply because they have identical dimensions.
32. Inspection of Large Sapphire Windows
A complete inspection plan may include:
Material
- material certification;
- crystal orientation.
Dimensions
- diameter;
- length/width;
- thickness;
- bevel/chamfer;
- clear aperture.
Surface
- scratches;
- digs;
- chips;
- polishing defects.
Geometry
- flatness;
- parallelism;
- wedge;
- TTV.
Optical
- spectral transmission;
- coating performance;
- transmitted wavefront.
Edge
- edge chips;
- cracks;
- chamfer dimensions.
Cleanliness
- particles;
- stains;
- packaging contamination.
A pre-shipment sapphire-window inspection should be matched to the customer’s agreed drawing and acceptance method rather than relying on generic “optical grade” terminology.
33. Interferometric Inspection
Flatness is commonly measured using an interferometer.
For a large aperture, important test conditions include:
- reference flat size;
- support fixture;
- test wavelength;
- clear aperture;
- analysis method.
The inspection report may include:
- PV;
- RMS;
- power;
- irregularity;
- astigmatism.
A supplier and customer should agree whether:
λ/4
means total surface PV or another defined parameter.
Otherwise two laboratories can report different results for the same component.
34. Transmitted Wavefront Test
For high-quality EO/IR windows, a transmitted wavefront test can be especially valuable.
The test beam passes through the sapphire.
The resulting error includes the combined effect of:
- both surfaces;
- thickness variation;
- crystal;
- stress.
This makes it closer to actual system performance than a single-surface flatness test.
For large imaging windows, it can identify problems that ordinary cosmetic inspection cannot detect.
35. Surface Roughness Inspection
Potential measurement methods include:
- white-light interferometry;
- optical profilometry;
- AFM.
For general imaging systems, extremely low roughness may not always be necessary.
For:
- low-scatter optics;
- short wavelengths;
- sensitive detectors;
roughness becomes more important.
The requirement should be linked to system performance.
36. Edge Inspection
The complete circumference should be inspected.
Possible acceptance criteria include:
- maximum chip size;
- no radial cracks;
- bevel continuity;
- no sharp corners;
- no chips entering clear aperture.
For rectangular windows, corners deserve special attention.
A small edge defect can be mechanically more important than a relatively large cosmetic defect in a non-optical edge region.
37. Stress Inspection
Large sapphire windows can also be examined under polarized light.
This can help identify:
- residual stress;
- mounting-induced stress;
- crystal patterns.
For finished assemblies, comparing the sapphire:
before mounting
and:
after mounting
can reveal whether the housing is deforming the window.
This is particularly useful when unexpected wavefront degradation appears after assembly.
38. Inspection Before and After Mounting
For a demanding sensor program, consider two inspection stages.
Stage 1 — Free Window
Inspect:
- dimensions;
- flatness;
- wavefront;
- coating;
- edge quality.
Stage 2 — Mounted Assembly
Recheck:
- transmitted wavefront;
- alignment;
- stress;
- optical transmission.
If the free window passes but the mounted assembly fails, the problem is likely not the polishing process.
It may be:
- retaining force;
- gasket geometry;
- housing flatness;
- thermal stress.
This distinction can save substantial troubleshooting time.
39. Example Specification — 150mm Industrial EO/IR Window
Material: Optical-grade sapphire
Orientation: C-plane
Outside Diameter: 150.0 ±0.10 mm
Thickness: 5.0 ±0.10 mm
Clear Aperture: ≥135 mm
Surface Quality: 40/20
Flatness: λ/4 @632.8 nm over clear aperture
Parallelism: ≤30 arc sec
Surface Roughness: Ra ≤1 nm
Edges: Fine ground
Bevel: 0.3 × 45°
Coating: Broadband AR
Wavelength: 3–5 µm
AOI: 0°
Application: Industrial MWIR thermal imaging
Quantity: 10 prototype / production forecast
The exact thickness should still be confirmed from the mounting and mechanical conditions.
40. Example Specification — Rectangular Process-Monitoring Window
Material: Single-crystal sapphire
Size: 180 × 120 mm
Thickness: 8 mm
Corner Radius: R5 mm
Clear Aperture: 160 × 100 mm
Surface Quality: 40/20
Flatness: λ/2 @632.8 nm
Parallelism: ≤1 arcmin
Edge: Fine ground + protective chamfer
Optical Band: 400–1000 nm
Coating: Broadband visible/NIR AR
Operating Temperature: 200°C
Housing Material: Stainless steel
Mounting: Compliant gasket + retaining ring
Application: Industrial high-temperature process monitoring
For this design, thermal-expansion clearance should be evaluated before finalizing the housing.
41. Example Specification — High-Resolution Sensor Window
Material: Optical sapphire
Orientation: C-plane
Diameter: 120 mm
Thickness: 4 mm
Clear Aperture: 108 mm
Surface Quality: 20/10
Surface Flatness: λ/10 @632.8 nm
Transmitted Wavefront: ≤λ/4
Parallelism: ≤10 arc sec
Ra: ≤0.5 nm
Coating: Dual-band AR
Optical Bands: 450–700 nm + 3–5 µm
Mounting: Low-stress compliant mount
Application: Multispectral scientific imaging
This is a much more demanding component than a simple protective sapphire cover.
42. RFQ Checklist for Large-Aperture Sapphire Windows
When requesting a quotation, provide:
Material
- Sapphire grade
- Crystal orientation
Dimensions
- OD or length × width
- Thickness
- Dimensional tolerances
- Corner radius if rectangular
Optical Aperture
- Clear aperture
- Coating aperture
Optical Quality
- Surface quality
- Flatness
- Transmitted wavefront
- Parallelism / wedge
- Surface roughness
Spectral Requirement
- Visible
- NIR
- SWIR
- MWIR
- exact wavelength band
Coating
- Uncoated
- AR
- BBAR
- dual-band AR
- required reflection/transmission
- AOI
Mechanical Conditions
- Mounting structure
- Support diameter
- pressure differential
- vibration
- window orientation
Temperature
- operating temperature
- thermal cycling range
- housing material
Edge
- ground/polished
- bevel/chamfer
- maximum chip size
Inspection
- interferometer report
- transmission report
- coating curve
- material certification
- dimensional report
Quantity
- prototype
- qualification
- production
This information allows the window to be designed around the actual system rather than simply manufacturing a larger sapphire disc.
43. Common Design Mistakes
Mistake 1 — Scaling a Small Window Directly to a Larger Diameter
Mechanical deflection does not scale linearly.
Mistake 2 — Specifying OD but Not Clear Aperture
The unsupported area is critical to structural design.
Mistake 3 — Using Published Sapphire Strength as Allowable Design Stress
Real strength is strongly influenced by edge and surface defects.
Mistake 4 — Over-Clamping the Window
Mounting stress can destroy excellent optical flatness.
Mistake 5 — Ignoring CTE Difference Between Sapphire and Housing
This can generate thermal stress.
Mistake 6 — Measuring Flatness Before Coating Only
Coating stress can change the surface figure.
Mistake 7 — Specifying Only Surface Flatness for an Imaging System
Transmitted wavefront may be the more useful system specification.
Mistake 8 — Ignoring Edge Finish
A large sapphire part can fail from a tiny edge crack.
44. How to Reduce Cost Without Sacrificing Performance
Large sapphire windows can become expensive quickly.
Cost can often be controlled by avoiding unnecessary requirements.
For example:
Reduce Clear Aperture
Do not require the optical region to extend unnecessarily close to the edge.
Use Appropriate Surface Quality
40/20 may be sufficient where 20/10 provides no system benefit.
Avoid Excessive Flatness
λ/4 may be adequate instead of λ/10.
Define Functional Areas
Allow mounting zones to remain ground or uncoated.
Provide Realistic Edge-Chip Limits
Do not require perfect cosmetic edges if they are outside the optical and sealing zones.
Use Prototype Qualification
Confirm system performance before committing to the tightest production specifications.
The most economical specification is the one that matches the actual optical error budget.
Conclusion
Large-aperture sapphire windows provide an excellent combination of:
**optical transparency
- mechanical durability
- scratch resistance
- chemical stability
- infrared capability**
for EO/IR sensors and other demanding optical systems.
But as aperture increases, the design changes fundamentally.
The critical relationship becomes:
aperture
→ thickness
→ stiffness
→ flatness
→ mounting stress
→ edge condition
→ transmitted wavefront
→ final image quality
A high-quality large sapphire window therefore requires more than good polishing.
Its performance depends on the complete system:
material
→ crystal orientation
→ geometry
→ edge preparation
→ polishing
→ coating
→ mounting
→ inspection
Mounting design deserves particular attention because a precisely polished window can be distorted after installation by excessive retaining force, gasket compression or thermal-expansion mismatch.
Likewise, the mechanical strength of sapphire should not be evaluated from bulk material data alone. Surface polish, edge damage and mounting conditions can significantly influence practical strength.
For EO/IR imaging systems, large sapphire windows should therefore be specified using both optical and mechanical parameters.
ZMSH Sapphire Windows can evaluate custom large-aperture sapphire components for:
- industrial EO/IR sensors;
- MWIR thermal imaging;
- semiconductor equipment;
- high-temperature monitoring;
- machine vision;
- spectroscopy;
- scientific instruments;
- harsh-environment optical systems.
Customers can provide the drawing, sapphire orientation, outside dimensions, clear aperture, thickness, mounting method, operating temperature, wavelength, surface quality, flatness, transmitted wavefront, coating and quantity for technical evaluation and quotation.
FAQ
How thick should a large sapphire window be?
There is no universal thickness. It depends on clear aperture, unsupported diameter, pressure difference, support geometry, temperature and allowable optical deformation. Thickness should be evaluated for the actual mounting condition.
Is surface flatness the same as transmitted wavefront?
No. Surface flatness describes one surface, while transmitted wavefront includes the combined effects of both surfaces, thickness variation, crystal properties and stress. For precision EO/IR imaging, transmitted wavefront can be more meaningful.
Can sapphire windows be made around 150mm diameter?
Yes. Commercial optical sapphire windows are currently available at approximately 150 mm diameter, demonstrating that this size is practical for precision optical production.
Why does mounting affect sapphire window flatness?
Large or thin sapphire windows can bend when compressed by retaining rings, O-rings, adhesives or uneven supports. Mounting stress can therefore change both flatness and transmitted wavefront.
Why is edge quality important?
Sapphire is brittle, so chips and microcracks at the edge can become fracture initiation points. Fine grinding, beveling and controlled chip limits improve handling and structural reliability.
Should a large sapphire window use AR coating?
Usually when transmission is important. Sapphire’s relatively high refractive index causes significant uncoated Fresnel reflection. AR coatings can substantially improve transmission and can be optimized for visible, NIR or 2–5 µm infrared bands.
What optical quality is suitable for an industrial EO/IR window?
It depends on the sensor. 40/20 surface quality and λ/4 or λ/2 flatness may be sufficient for many industrial systems, while precision imaging may require 20/10, λ/10 or controlled transmitted wavefront.
What information should be included in a large sapphire window RFQ?
Provide overall size, clear aperture, thickness, sapphire orientation, optical wavelength, surface quality, flatness, transmitted wavefront if needed, parallelism, coating, mounting method, housing material, operating temperature, pressure conditions and quantity.