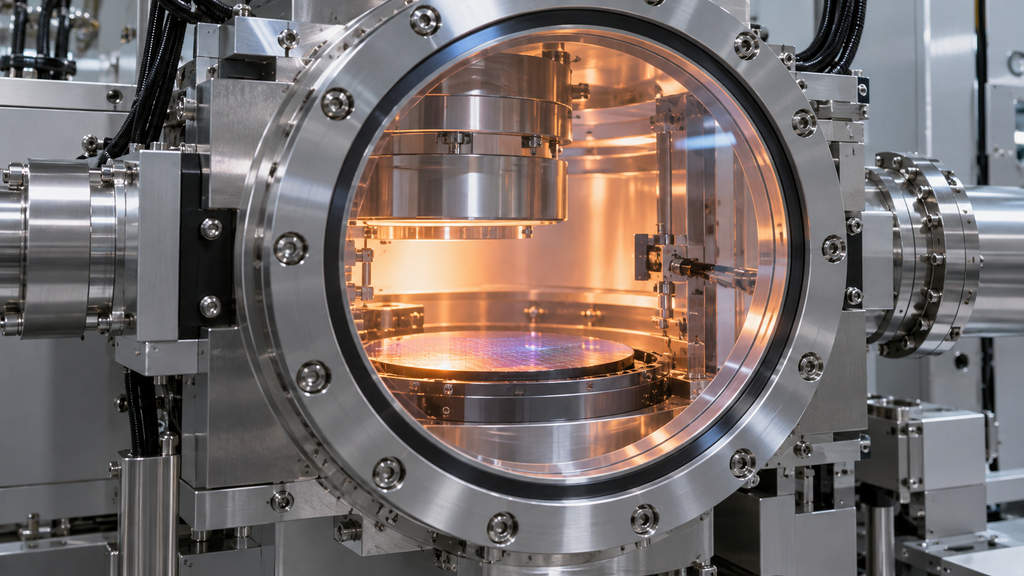
As semiconductor equipment becomes larger, more automated and more optically sophisticated, the size of protective optical windows is also increasing.
Large sapphire windows may be used in:
- Wafer inspection systems
- Advanced packaging equipment
- Plasma process chambers
- Vacuum equipment
- Optical metrology systems
- Machine-vision modules
- Laser process equipment
- High-temperature monitoring systems
- Large-area substrate inspection
- Process observation ports
At small dimensions, sapphire-window design can appear relatively straightforward.
Specify:
diameter or length × width × thickness
then add the required optical polish.
As the window becomes larger, however, this approach becomes increasingly risky.
A large sapphire window behaves differently from a small optic because several engineering effects increase rapidly with size:
- Deflection becomes more significant
- Thickness becomes structurally critical
- Flatness becomes more difficult to maintain
- Mounting stress becomes more important
- Pressure loading increases
- Temperature gradients can become larger
- Edge and corner defects become more dangerous
- Coating and polishing uniformity become harder to control
For advanced semiconductor equipment, the window must therefore be treated as both:
an optical component
and
a structural component.
This article explains the most important considerations when specifying large sapphire windows, with particular attention to thickness scaling, flatness, mounting stress and thermal shock.
1. What Is Considered a Large Sapphire Window?
There is no single dimension at which a sapphire window officially becomes “large.”
The practical definition depends on:
- Shape
- Thickness
- Clear aperture
- Optical specification
- Pressure loading
- Manufacturing capability
A 100 mm diameter window may be relatively easy for one application but highly demanding if the specification also requires:
- Very thin thickness
- Tight flatness
- 10-5 surface quality
- Tight transmitted wavefront
- High pressure differential
Likewise, a 200 × 50 mm rectangular sapphire window may be mechanically more challenging than a compact 120 × 120 mm part because of its aspect ratio.
The term large sapphire window should therefore be understood as a component whose dimensions make mechanical and optical scaling effects important.
2. Why Semiconductor Equipment Is Driving Larger Optical Apertures
Several semiconductor-equipment trends can increase the required viewing area.
These include:
- Larger wafer and substrate formats
- Advanced packaging
- Panel-level processing
- Large-area machine vision
- Multi-camera inspection
- Line-scan inspection
- Automated optical inspection
- Large process chambers
- Expanded laser scanning fields
A larger viewing area can reduce the need to mechanically reposition the optical system or target.
However, increasing the clear aperture is not free.
When window dimensions grow, the optic must maintain:
- Mechanical stability
- Optical flatness
- Surface quality
- Alignment
- Environmental durability
over a much larger area.
This is where thickness scaling becomes important.
3. Thickness Cannot Simply Be Scaled Linearly
A common mistake is to assume:
If a 50 mm window works at 2 mm thickness, a 100 mm window should work at 4 mm thickness.
Real plate behavior is more complicated.
Mechanical deflection depends strongly on:
- Unsupported span
- Thickness
- Elastic modulus
- Boundary conditions
- Pressure differential
- Aspect ratio
Thickness has a very strong effect on plate stiffness.
This means increasing thickness slightly can substantially improve rigidity.
At the same time, increasing window diameter or unsupported span can rapidly increase deflection.
Therefore, large-window thickness should be determined through mechanical analysis rather than simple proportional scaling.
4. Overall Size and Unsupported Aperture Are Different
The mechanical size that matters most is often not the outer dimension of the sapphire.
Consider a window with:
Overall diameter: 180 mm
but:
Unsupported clear opening: 140 mm
The outer 20 mm perimeter on each side may be supported by the housing.
Mechanically, the relevant unsupported span is closer to 140 mm than 180 mm.
The same principle applies to rectangular windows.
For example:
Overall size: 200 × 120 mm
but
Unsupported aperture: 170 × 90 mm
The mechanical calculation should use the real support geometry.
This is why a customer RFQ should ideally include the window mount or at least the unsupported aperture.
5. Thickness Affects More Than Mechanical Strength
Increasing sapphire thickness improves stiffness, but thickness also influences optical and thermal behavior.
A thicker window can result in:
- Greater optical path length
- More material cost
- Higher mass
- Increased thermal mass
- Greater temperature difference through thickness
- More difficult polishing
- Potentially more demanding coating handling
The optimum thickness is therefore not simply:
as thick as possible.
It should provide adequate mechanical stability without creating unnecessary optical or thermal penalties.
6. Thin Large Windows Are Particularly Challenging
A large thin sapphire plate can be attractive because it reduces weight and material use.
However, as the ratio of span to thickness increases, the optic becomes increasingly sensitive to:
- Gravity
- Pressure
- Mounting force
- Temperature
- Handling
A thin large window may satisfy dimensional inspection when placed horizontally on a metrology fixture but deform when installed vertically or under vacuum.
This is why the installed operating condition should be considered from the beginning.
7. Flatness Becomes Harder as Aperture Increases
Maintaining optical flatness over a small area is easier than maintaining it over a large aperture.
A larger optic must be polished while controlling:
- Global curvature
- Local high and low areas
- Edge roll-off
- Thickness variation
- Surface stress
For semiconductor optical systems, flatness may be specified in terms such as:
- λ
- λ/2
- λ/4
- λ/10
at a defined reference wavelength.
However, a specification without aperture size can be misleading.
For example:
λ/4 over Ø30 mm
is very different from:
λ/4 over Ø180 mm
The second requirement is considerably more demanding.
8. Flatness Should Be Specified Over the Clear Aperture
For large sapphire windows, it is often unnecessary to maintain the strictest optical specification all the way to the physical edge.
A practical design may specify:
Overall size: 180 mm
Clear aperture: 160 mm
Flatness: λ/4 over clear aperture
The outer zone can then be reserved for:
- Mounting
- Bevel
- Gasket
- Retaining ring
- Edge support
This can improve both manufacturability and reliability.
9. Free-State Flatness Is Not Installed Flatness
This distinction becomes extremely important for large optics.
A window may measure:
λ/4 flatness
when resting freely on an optical test fixture.
After installation, the metal frame may apply uneven stress.
The actual optical surface may then become:
- Slightly bowed
- Twisted
- Locally distorted
The sapphire itself has not changed permanently.
The mounting condition has changed the shape.
For precision semiconductor metrology, the engineer should therefore distinguish between:
free-state optical specification
and
mounted-state system performance.
10. Mounting Stress Can Distort a Precision Window
Sapphire is stiff, but a sufficiently large window can still be elastically distorted.
Sources of mounting stress include:
- Uneven screw torque
- Non-flat housing
- Excessive gasket compression
- Metal-to-sapphire point contact
- Thermal expansion mismatch
- Tight dimensional fit
- Retaining-ring preload
A common failure mode is to manufacture an extremely flat sapphire window and then bolt it tightly against a housing that is less flat than the optic.
The sapphire is forced to conform to the metal.
This can destroy the optical advantage of the high-quality window.
11. The Housing Must Be Designed to the Same Philosophy
For high-precision semiconductor equipment, the mounting frame should be considered part of the optical system.
Important housing characteristics include:
- Seating-surface flatness
- Surface finish
- Support width
- Corner geometry
- Screw placement
- Gasket design
- Thermal expansion
- Structural stiffness
A high-quality sapphire window cannot compensate for a poorly designed housing.
12. Uniform Perimeter Support Is Often Preferable
For many large windows, distributed support around the perimeter is preferable to a few concentrated clamping points.
Concentrated loading can create local bending stress.
A perimeter support can spread the load more evenly.
However, support must still be controlled.
A rigid full-perimeter clamp can also create stress if:
- The frame is warped
- The gasket thickness varies
- The thermal expansion differs significantly
The goal is not maximum clamping force.
The goal is stable positioning with controlled preload.
13. Gaskets Can Reduce Stress—If Selected Correctly
A compliant gasket can perform several functions:
- Distribute load
- Protect the sapphire edge
- Compensate for small housing irregularities
- Provide sealing
- Allow differential thermal expansion
But gasket selection becomes more demanding in semiconductor equipment.
The material may need to satisfy requirements related to:
- Vacuum compatibility
- Outgassing
- Temperature resistance
- Plasma compatibility
- Chemical resistance
- Particle generation
A soft elastomer appropriate for a conventional industrial machine may not be acceptable inside a semiconductor process system.
14. Tight Mechanical Fits Should Be Avoided
A large sapphire window should generally not be trapped tightly between rigid metal walls with no expansion allowance.
During temperature changes, the metal housing and sapphire expand differently.
If there is insufficient clearance, the sapphire can experience compressive edge loading.
This may lead to:
- Distortion
- Edge damage
- Fracture
Assembly clearance should therefore account for:
- Manufacturing tolerance
- Temperature range
- Differential thermal expansion
The exact value must be determined for the actual materials and geometry.
15. Sapphire Is Strong but Brittle
Sapphire has excellent hardness and high mechanical strength compared with many conventional optical materials.
However, it remains brittle.
Its practical strength is influenced by:
- Surface defects
- Edge chips
- Grinding damage
- Corner defects
- Scratches
- Mounting stress
This is why the edge quality of a large window can be just as important as its central optical polish.
16. Edge Defects Become More Important as Size Increases
A larger window has more perimeter length.
That means more opportunity for:
- Edge chips
- Microcracks
- Handling damage
A small defect can become a fracture initiation point when the component is mechanically loaded.
For this reason, large sapphire windows should have controlled:
- Edge finish
- Protective bevel
- Corner geometry
- Chip acceptance criteria
17. Protective Bevels
A protective bevel removes the sharp intersection between the polished face and the outer edge.
This can reduce vulnerability during:
- Shipping
- Cleaning
- Coating
- Installation
The bevel should be large enough to protect the edge but small enough to remain outside the optical clear aperture.
Typical drawings specify the bevel separately from the overall window size.
18. Rectangular Large Windows Need Corner Control
Large rectangular sapphire windows introduce an additional issue:
corners.
Perfectly sharp 90° corners can increase handling difficulty.
Depending on the housing, it may be better to specify:
- Small radius
- Corner chamfer
- Controlled edge break
A rounded corner can reduce localized stress and improve manufacturability.
However, the corner geometry must also match the machined housing pocket.
19. Pressure Differential Can Dominate the Design
Some semiconductor windows separate:
vacuum
from
atmosphere.
In this situation, the window experiences a continuous pressure differential.
As aperture size increases, the total load also increases.
This can lead to:
- Elastic deflection
- Optical distortion
- Mechanical stress
For vacuum equipment, window thickness should therefore be evaluated with the actual:
- Aperture
- Support condition
- Pressure differential
- Safety factor
A generic thickness recommendation is not sufficient.
20. Pressure-Induced Deflection Can Affect Imaging Before Failure
A window does not need to break before it becomes a problem.
Imagine a large sapphire viewport under vacuum.
It may deflect slightly toward the vacuum side.
Mechanically, this may be completely safe.
Optically, however, the curvature can alter:
- Focus
- Wavefront
- Image geometry
- Laser beam direction
Therefore, pressure-loaded windows sometimes require a stricter deflection limit than the structural-strength limit.
This is particularly relevant for:
- Interferometry
- Precision imaging
- Machine vision
- Laser metrology
21. Structural Requirement and Optical Requirement May Be Different
Two calculations should often be considered.
Structural Requirement
Will the sapphire remain safely below the allowable mechanical stress?
Optical Requirement
Will the deflection remain small enough that the imaging or laser system still performs correctly?
The optical requirement can sometimes dictate a thicker window than mechanical strength alone would require.
22. Thermal Shock Is a System-Level Problem
Sapphire performs well at elevated temperature, but thermal-shock performance depends on much more than material name.
Important variables include:
- Window thickness
- Size
- Temperature difference
- Heating rate
- Cooling rate
- Mounting
- Surface condition
- Edge defects
A large window may develop a significant temperature gradient because one area heats faster than another.
This can create internal stress even when the maximum temperature itself is within sapphire’s material capability.
23. Why Large Windows Are More Sensitive to Temperature Gradients
A small optical window may reach a relatively uniform temperature quickly.
A large window can experience different temperatures at different positions.
For example:
center exposed to hot process radiation
while
edge remains cooled by the metal housing.
This creates a radial temperature gradient.
Another example:
process side hot
while
external camera side remains cooler.
This creates a through-thickness gradient.
Both can generate thermal stress.
24. Edge Cooling Can Be Significant
The sapphire perimeter is often in direct contact with a metal mount.
The metal structure may act as a heat sink.
As a result:
- The center heats rapidly
- The edge remains cooler
For large windows, the distance between the hot center and cooled edge can become substantial.
The mounting design should therefore consider thermal conduction, not just mechanical support.
25. Thicker Windows Can Create Larger Through-Thickness Gradients
Increasing thickness improves stiffness.
But it also increases the distance heat must travel through the sapphire.
During rapid temperature change, the hot-side surface and cold-side surface may temporarily be at different temperatures.
This creates thermal stress.
Therefore, increasing thickness is not always an unrestricted solution to every mechanical problem.
The correct design balances:
stiffness + thermal behavior + optical requirement.
26. Thermal Shock Depends on Heating Rate
A window held continuously at a high stable temperature may experience less thermal stress than the same window subjected repeatedly to rapid heating and cooling.
Equipment designers should therefore provide:
- Maximum operating temperature
- Minimum operating temperature
- Ramp rate
- Number of cycles
- Hot-zone distribution
when thermal shock is a concern.
Simply stating:
Operating temperature = 500°C
does not describe the complete thermal environment.
27. Repeated Thermal Cycling Can Reveal Weaknesses
A large sapphire window may survive initial installation but develop problems after many process cycles.
Possible issues include:
- Edge microcrack propagation
- Coating degradation
- Seal deterioration
- Mounting-stress accumulation
Qualification testing should therefore reflect actual use.
For demanding semiconductor tools, useful testing may include repeated:
heat → soak → cool
cycles.
28. Thermal Expansion Mismatch With Metal Frames
Sapphire and common housing metals have different coefficients of thermal expansion.
During heating, the frame may expand more than the sapphire.
If the mount allows movement, this can be manageable.
If the sapphire is rigidly constrained, differential expansion can create mechanical stress.
Potential solutions include:
- Radial clearance
- Compliant gasket
- Spring loading
- Controlled retaining structures
The exact solution depends on:
- Housing material
- Temperature
- Window size
29. Avoid Metal-to-Sapphire Point Contact
A hard metal point pressing against the sapphire edge can create very high local stress.
This is especially undesirable for large windows.
Contact should be distributed where possible.
During assembly, also avoid:
- Burrs
- Sharp screws
- Machining debris
near the sapphire edge.
A tiny metal burr can locally concentrate load and damage an otherwise high-quality optic.
30. Surface Quality Still Matters on Large Windows
Large sapphire windows are often used for imaging or laser monitoring.
Surface quality can therefore affect:
- Scattering
- Contrast
- Stray light
- Laser performance
Typical scratch-dig specifications may include:
- 60-40
- 40-20
- 20-10
depending on application.
The entire large surface does not always require the tightest optical grade.
A defined clear aperture can help balance optical performance and cost.
31. Large Optical Areas Increase Inspection Difficulty
A small defect on a 20 mm window is easy to locate.
A large sapphire plate may contain a much larger inspection area.
The probability of finding:
- Cosmetic defects
- Surface contamination
- Local coating variation
naturally increases with area.
This is another reason extremely tight cosmetic requirements can significantly increase cost as part size increases.
32. Surface Roughness
For precision optical applications, surface roughness can influence:
- Scatter
- Laser transmission
- Coating performance
However, roughness specification should match the application.
Machine-vision protection may tolerate a different surface than:
- Interferometry
- High-power laser
- Short-wavelength inspection
A low roughness value should not be specified purely for marketing reasons.
33. Transmitted Wavefront Error
For large windows used in precision metrology, transmitted wavefront can be more important than surface flatness alone.
Wavefront distortion can arise from:
- Surface figure
- Thickness variation
- Material properties
- Mounting deformation
A large-window drawing may therefore specify both:
surface flatness
and
transmitted wavefront error.
The actual requirement should follow the optical system.
34. Parallelism
Large windows often use parallel optical surfaces.
Poor parallelism can cause beam deviation.
For camera systems, this may introduce a small image offset.
For laser metrology, the effect may be more significant.
Parallelism should therefore be specified when the optical path is sensitive to angular deviation.
Again, overly tight values should be avoided when they provide no system benefit.
35. Large Windows May Require AR Coating
An uncoated sapphire surface reflects part of the incident light.
For a two-surface window, these losses can reduce transmission and introduce reflections.
AR coating may be used to improve:
- Throughput
- Image contrast
- Laser efficiency
- Stray-light performance
The coating should be designed for the actual wavelength range.
36. Large-Area Coating Uniformity
Coating a large sapphire window introduces its own manufacturing challenge.
The coating must remain uniform across the clear aperture.
Potential variables include:
- Layer thickness
- Reflectance
- Transmission
- Color shift
- Stress
Large coated optics may therefore require mapping or multi-position spectral measurement.
The required inspection method should be agreed before production.
37. Coating Stress Can Influence Large Thin Windows
Thin-film coatings can have residual stress.
On a thick small optic, the effect may be negligible.
On a very large thin window, coating stress may contribute to small changes in flatness.
This is especially relevant when:
- Coating only one side
- Using thick multilayer stacks
- Requiring very tight flatness
For precision applications, coating design and mechanical geometry should therefore be considered together.
38. Coating Both Sides
Applying similar coatings to both sides can sometimes help maintain optical balance, although actual stress depends on the coating design.
The main optical reason for double-sided AR coating is to reduce reflection from both interfaces.
A drawing should clearly identify:
Surface 1
and
Surface 2
with the required coating on each.
39. Crystal Orientation
Sapphire is anisotropic.
For precision optical systems, crystal orientation can influence:
- Refractive index
- Birefringence
- Mechanical behavior
C-plane sapphire is commonly used for optical windows.
For large precision components, the RFQ should specify the required orientation rather than simply requesting:
sapphire glass.
40. Material Quality Becomes More Important With Area
A large optical component requires a larger usable region of sapphire material.
The manufacturer must therefore consider:
- Crystal quality
- Inclusions
- Internal defects
- Stress
- Orientation uniformity
A material defect that can be positioned outside a 20 mm window may fall inside the clear aperture of a 180 mm window.
Large-area optical blanks therefore require careful material selection.
41. Large Circular vs Large Rectangular Windows
The two geometries behave differently.
Circular Window
Advantages include:
- Symmetric stress distribution
- Convenient sealing
- Easier rotational alignment
Rectangular Window
Advantages include:
- Efficient use of rectangular field of view
- Compatibility with machine vision
- Better use of limited housing space
But rectangular windows introduce:
- Corners
- Direction-dependent bending
- Aspect-ratio effects
Thickness and support design should therefore not be copied directly between shapes.
42. Large Sapphire Windows for Wafer Inspection
A large sapphire window may protect optical components in a wafer-inspection system.
Potential requirements include:
- High transmission
- Low distortion
- Large field of view
- Stable flatness
- Low particle contamination
- AR coating
The system may inspect:
- Wafer surface defects
- Edge defects
- Pattern variation
- Bonded wafers
- Advanced packaging substrates
The window must not introduce artifacts that could be mistaken for defects.
43. Large Windows for Machine Vision
Machine-vision systems may require:
- Wide camera field
- Multiple cameras
- Large illumination area
A large rectangular sapphire window can protect the imaging system while allowing a broad field of view.
For these applications, important parameters may include:
- Flatness
- Parallelism
- AR coating
- Surface quality
- Mechanical mounting
The window should be included in the camera optical model rather than added after system calibration.
44. Large Sapphire Windows for Plasma Equipment
Plasma process equipment creates additional requirements.
The window may experience:
- Vacuum
- Heat
- Plasma exposure
- Chemical species
- Repeated cleaning
Sapphire can provide strong mechanical and optical performance in such environments, but the complete compatibility must still be evaluated.
The coating, seal and mounting hardware may have lower environmental limits than the sapphire itself.
45. Large Windows for Laser Process Monitoring
Laser-based semiconductor tools may use optical windows for:
- Beam delivery
- Alignment
- Process monitoring
- Endpoint detection
For these applications, large sapphire windows may need additional specifications such as:
- Laser-induced damage threshold
- Transmitted wavefront
- Low scatter
- Specialized AR coating
If high laser power is involved, contamination control becomes especially important because particles can create localized absorption.
46. Gravity Can Matter During Metrology
For very large thin windows, orientation during measurement can matter.
An optic measured horizontally may sag slightly under its own weight.
The same optic mounted vertically experiences gravity differently.
When flatness tolerances are extremely tight, the supplier and customer should agree on:
- Measurement orientation
- Support points
- Inspection method
Otherwise, two different measurements can produce slightly different results.
47. Support During Shipping
Large sapphire windows require careful packaging.
Although sapphire is hard, a large plate can still be damaged by:
- Edge impact
- Point loading
- Vibration
- Contact with another part
Packaging should provide:
- Edge protection
- Face separation
- Distributed support
- Clean environment
Optical surfaces should not carry mechanical packaging load.
48. Handling
Large windows may require two-person or fixture-assisted handling depending on size.
Workers should avoid gripping only one corner or applying uneven bending force.
For coated surfaces, direct contact with the clear aperture should be avoided.
Handling procedures should treat the component as both:
precision optic
and
brittle structural part.
49. Cleaning Large Sapphire Windows
Cleaning becomes more difficult as area increases.
Potential problems include:
- Streaks
- Residue
- Particle redeposition
- Uneven drying
For semiconductor equipment, cleaning procedures should be controlled.
The compatibility of cleaning chemistry with:
- Sapphire
- AR coating
- Edge treatment
must also be confirmed.
50. Cleanliness Can Affect Inspection Accuracy
In wafer inspection, a contaminant on the window can appear in the image.
Depending on focus position, it may create:
- Blurred feature
- Dark spot
- Scattered light
- False defect
The machine-vision algorithm may then classify a window contaminant as a wafer defect.
Therefore, window cleanliness becomes part of metrology stability.
51. Large Clear Apertures Need Maintenance Access
Equipment designers should consider how the window will be:
- Cleaned
- Inspected
- Replaced
A design that provides excellent optical access but makes window maintenance impossible can increase equipment downtime.
Large windows should therefore be integrated with serviceability in mind.
52. Example Large Circular Window RFQ
A practical RFQ might include:
Product: Large Sapphire Optical Window
Application: Semiconductor Wafer Inspection
Material: Optical-Grade Sapphire
Crystal Orientation: C-Plane
Outer Diameter: Ø180 mm
Thickness: Customer specified after mechanical evaluation
Clear Aperture: Ø160 mm minimum
Surface Quality: 20-10 scratch-dig
Flatness: According to optical drawing
Parallelism: Customer specified
Transmitted Wavefront: If required
Coating: AR both surfaces
Wavelength: 450–700 nm
Edge: Fine ground with protective bevel
Environment: Clean semiconductor equipment
Mounting: Full-perimeter support
Quantity: Prototype followed by production
53. Example Large Rectangular Window RFQ
Product: Large Rectangular Sapphire Window
Application: Advanced Packaging Machine Vision
Material: Optical-Grade Sapphire
Size: 200 × 120 mm
Thickness: To be mechanically validated
Unsupported Aperture: 170 × 90 mm
Corner Radius: R2 mm
Clear Aperture: 165 × 85 mm
Surface Quality: 40-20 or customer specified
Flatness: Customer specified
Edges: Fine ground
Bevel: Protective bevel
Coating: Broadband AR
Operating Temperature: Customer specified
Pressure Differential: None / specified
Mount: Gasketed perimeter frame
This is much more useful than simply requesting:
200 × 120 × 3 mm sapphire plate.
54. Information Required for Vacuum Applications
If the window separates atmosphere and vacuum, the RFQ should also provide:
- Maximum pressure differential
- Unsupported aperture
- Support geometry
- Window orientation
- Operating temperature
- Required safety factor
- Maximum allowable optical deflection
These parameters are necessary for a meaningful engineering review.
55. Information Required for Thermal Applications
For high-temperature equipment, provide:
- Maximum temperature
- Minimum temperature
- Heating rate
- Cooling rate
- Temperature distribution
- Number of cycles
- Housing material
This allows the manufacturer and equipment designer to evaluate thermal stress and mounting compatibility.
56. Prototype the Complete Assembly
For a large sapphire window, prototype qualification should ideally include the actual:
window + gasket + retaining frame + housing
rather than the sapphire alone.
Tests can include:
- Optical flatness after mounting
- Leak performance
- Pressure deflection
- Thermal cycling
- Image quality
- Coating stability
This is particularly important because many problems originate from the assembly rather than the sapphire blank.
57. Measure Optical Performance After Installation
If the window is used in precision metrology, evaluate:
- Focus
- Image distortion
- Wavefront
- Laser position
- Background scatter
after installation.
A sapphire component that passes dimensional inspection but causes unacceptable mounted-state distortion still requires system-level optimization.
58. Large Sapphire Windows Should Be Co-Designed
The best results usually come from cooperation between:
- Optical engineer
- Mechanical engineer
- Equipment designer
- Sapphire manufacturer
The optical engineer defines:
- Flatness
- wavefront
- coating
- clear aperture
The mechanical engineer defines:
- Thickness
- support
- preload
- housing
The equipment engineer defines:
- temperature
- pressure
- process environment
The sapphire manufacturer evaluates:
- Blank availability
- polishing capability
- edge processing
- coating compatibility
This co-design approach is especially important for unusually large components.
59. Questions to Ask a Large Sapphire Window Manufacturer
Before placing an order, consider asking:
- What maximum sapphire size can be processed?
- What thickness range is practical at the required size?
- What clear aperture can be guaranteed?
- How is large-area flatness measured?
- Can transmitted wavefront be measured?
- How is edge roll-off controlled?
- What corner radius is recommended?
- What protective bevel can be provided?
- How is crystal orientation documented?
- Can large-area AR coating be applied uniformly?
- Is coating mapping available?
- How is the part supported during optical inspection?
- Can mounting-induced deformation be evaluated?
- Can vacuum or pressure conditions be reviewed?
- Can thermal cycling be performed?
- What packaging is used for large optical windows?
- Can dimensional and optical inspection reports be supplied?
60. Avoid One-Line Specifications
A specification such as:
“Need 200 mm sapphire window, 3 mm thick.”
leaves too many unanswered questions.
A useful engineering specification should also define:
- Clear aperture
- Shape
- Edge geometry
- Pressure
- Temperature
- Flatness
- Surface quality
- Coating
- Crystal orientation
- Mounting method
Without this information, it is difficult to determine whether 3 mm is:
- More than sufficient
- Appropriate
- Too thin
61. Design Principle: Scale the System, Not Just the Window
The most important design principle is:
When sapphire-window size increases, the entire optical-mechanical system must be reconsidered.
Do not simply enlarge the drawing.
A larger window changes:
- Structural stiffness
- Pressure load
- Thermal gradients
- polishing difficulty
- mounting sensitivity
- coating behavior
The support structure must scale with it.
The inspection method must scale with it.
The thermal design must scale with it.
And the optical tolerance should be justified over the larger aperture.
Conclusion
Large sapphire windows can provide durable, high-performance optical interfaces for advanced semiconductor equipment, including wafer inspection, machine vision, vacuum systems, plasma tools and laser process monitoring.
However, large size changes the engineering problem.
Performance depends on the interaction of:
window size + thickness + unsupported aperture + flatness + mounting stress + pressure + temperature + edge condition
Thickness must be selected through mechanical and optical analysis rather than simple proportional scaling.
Flatness must be specified over a clearly defined aperture.
Mounting structures should distribute force without deforming the optic.
Pressure-induced deflection should be evaluated not only for structural safety but also for optical performance.
Thermal gradients and differential expansion must be considered when the equipment experiences rapid or uneven temperature changes.
And because sapphire remains a brittle single crystal, edge quality, bevels and careful handling remain critical even though the material is extremely hard.
For custom projects, a complete RFQ should therefore provide:
overall dimensions, clear aperture, unsupported aperture, thickness target, flatness, surface quality, crystal orientation, coating, pressure differential, operating temperature and mounting configuration.
When these parameters are designed together, large sapphire windows can provide stable optical performance while surviving the demanding mechanical and thermal environments found in advanced semiconductor equipment.